What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
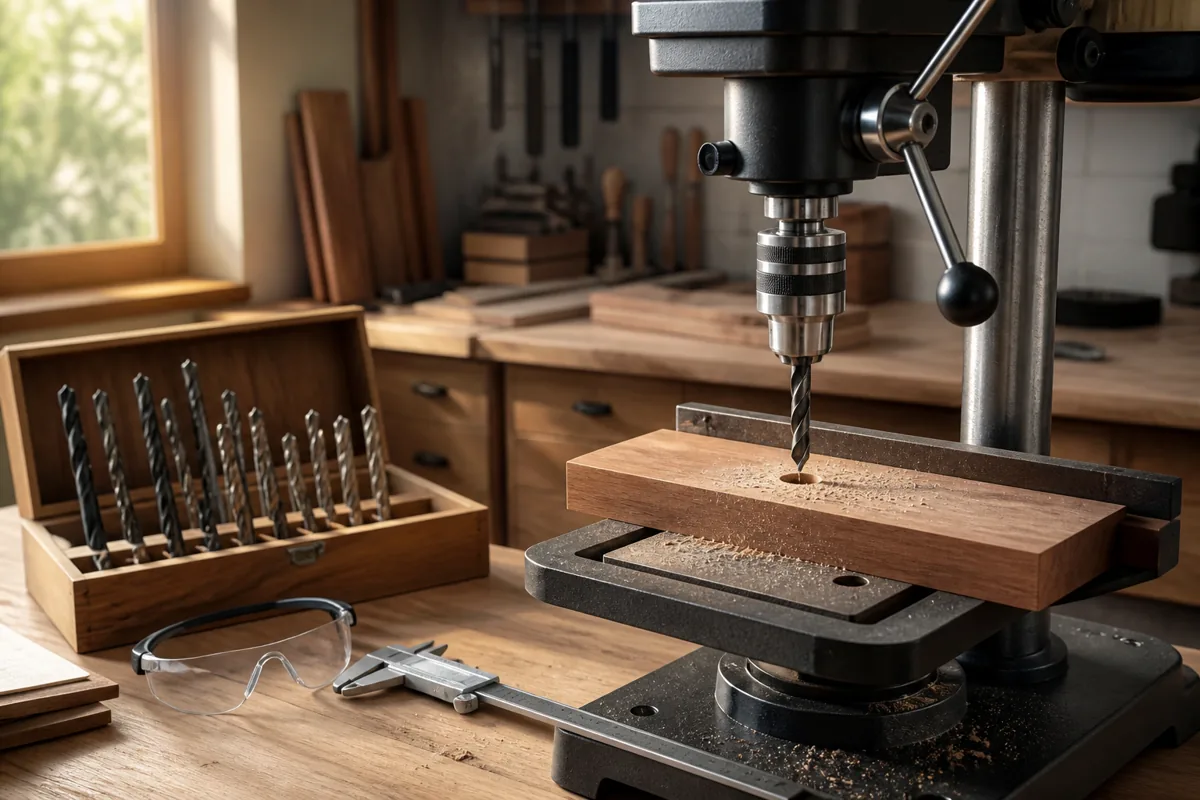
Accurate holes in metal brackets depend on more than a drill press’s advertised horsepower. The important details are a stiff table and column, low-speed control, a chuck that runs true, and a way to hold the bracket securely. For occasional work on small steel brackets, a compact benchtop press can be enough. For repeatable hole patterns or larger bits, rigidity and a useful low-speed range matter more than extra features.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.


Our Top Picks


What accuracy means on a drill press
For bracket work, accuracy has two parts: putting the hole in the right place and keeping it round and square. A press can drill straight down and still make a misplaced hole if the work shifts, the bit walks across the surface, or the table moves under load. Likewise, a cheap chuck with noticeable runout can leave a hole larger or rougher than expected.
Check the spindle and chuck for excessive side-to-side movement with the machine unplugged and the chuck empty. Some movement at the chuck’s outer end is not a direct measure of cutting accuracy, but obvious wobble is a warning. If the manufacturer publishes spindle runout or a test method, use that information to compare machines; don’t assume a larger motor means a more accurate press.
Features that matter for metal brackets
Steel needs slower speeds than wood. A useful press should have a low setting around 500 RPM or below for larger holes in mild steel, with higher settings available for small bits. The right speed depends on the bit diameter, steel type, and cutting tool. A small bit can run faster than a large hole saw, but overheating still dulls bits quickly. If a belt-drive press offers several pulley steps, changing speed takes time but is simple. Variable-speed controls are quicker to adjust, though they add cost and do not automatically make a machine more rigid.
Look for a table that locks firmly and can be squared to the spindle. A small table may be fine for a 2-inch bracket, but awkward when supporting long stock. A fence or angle vise can help repeat hole spacing, but it cannot replace clamping the work. Metal can catch and spin when a bit breaks through, so clamp the bracket to the table or to a drill-press vise. Never hold small steel parts by hand.
Depth stops are useful when drilling multiple holes to a consistent depth, though most bracket holes go through the material. A laser crosshair can help with rough positioning, but treat it as a convenience, not a precision measuring system. Mark the hole center with a layout tool and verify it before drilling.
Compare the main benchtop options
| Type | Best for | Trade-off |
|---|---|---|
| Compact belt-drive press | Occasional holes in thin brackets; tight budgets | Lower capacity and smaller table; speed changes require moving belts |
| Mid-size belt-drive press | Regular shop use and a wider range of bit sizes | Heavier and pricier; pulley changes still take time |
| Variable-speed benchtop press | Frequent changes between small and large bits | Costs more; electronic speed control is not a substitute for a rigid frame |
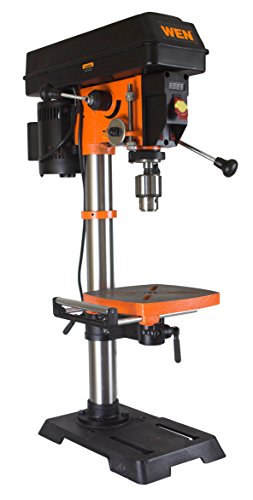
For a basic setup, compare benchtop drill presses suited to metal by low-speed range, spindle travel, table size, and published capacity—not by motor wattage alone. A 10- or 12-inch swing press is often a practical size for small brackets, but the required throat depth depends on how far the hole sits from the edge of your work.
Choosing a press for your workload
If you drill a few holes a month in mild steel under about 1/8 inch thick, a budget press can be perfectly adequate. Spend the savings on sharp bits, a center punch, cutting fluid, and a solid vise. For thicker plate, larger holes, or repeated production, choose a heavier press with a lower speed and a table that stays put under pressure. The cheap option becomes frustrating when it vibrates, slips out of square, or lacks the travel and clearance your brackets need.
Before buying, check the distance from the chuck to the column, the maximum distance from the spindle to the table, and the spindle stroke. These measurements determine whether a bracket will fit and whether the bit can reach the work without awkward setups. Also check whether the base has slots for bolting it to a bench. Bolting down a lightweight press can reduce movement, but it won’t fix a loose spindle or a flexible column.
For a repeatable setup, a drill-press vise for metalwork is a worthwhile accessory. Choose one with jaws wide enough for your brackets and a base that can be clamped or bolted down. A small vise is not useful if the part rocks above its jaws; add parallel supports or a sacrificial backing plate so the bracket sits flat.
A reliable method for accurate holes
Mark the hole location from a measured edge, then prick-punch the center. For larger holes, drill a small pilot hole first—often around 1/8 inch—rather than forcing a large bit to start from a flat surface. Secure the bracket, bring the bit down to check alignment, and adjust the work before switching the press on. Use cutting fluid where appropriate, feed steadily, and ease off as the bit breaks through. Excessive pressure can grab the part or snap a small bit; too little feed can rub and overheat the cutting edge.
If the hole location must be exact, test the setup on scrap of similar thickness. Measure from the same reference edge, and inspect the first hole before drilling a batch. A drill press makes it easier to keep holes square; it does not guarantee that hole spacing is right.
Common mistakes that spoil holes
Running a large bit too fast is a common cause of blue chips, smoke, and dull tooling. A bracket that is not clamped can spin violently, even if it feels secure under hand pressure. A dull bit may squeal and wander rather than cut cleanly. Finally, a tilted table can produce holes that are square to the table but not to the bracket face. Check table alignment with a square after adjusting the table, and recheck the clamp whenever you change the workpiece.
The best choice is the least expensive press that fits your stock, holds its setup, and has an appropriate low speed. For light, occasional bracket drilling, basic is fine. For frequent work where location and repeatability matter, put the budget toward rigidity, a sound chuck, and dependable clamping before paying extra for convenience features.