What's inside
As an Amazon Associate I earn from qualifying purchases. This post may contain affiliate links at no extra cost to you.
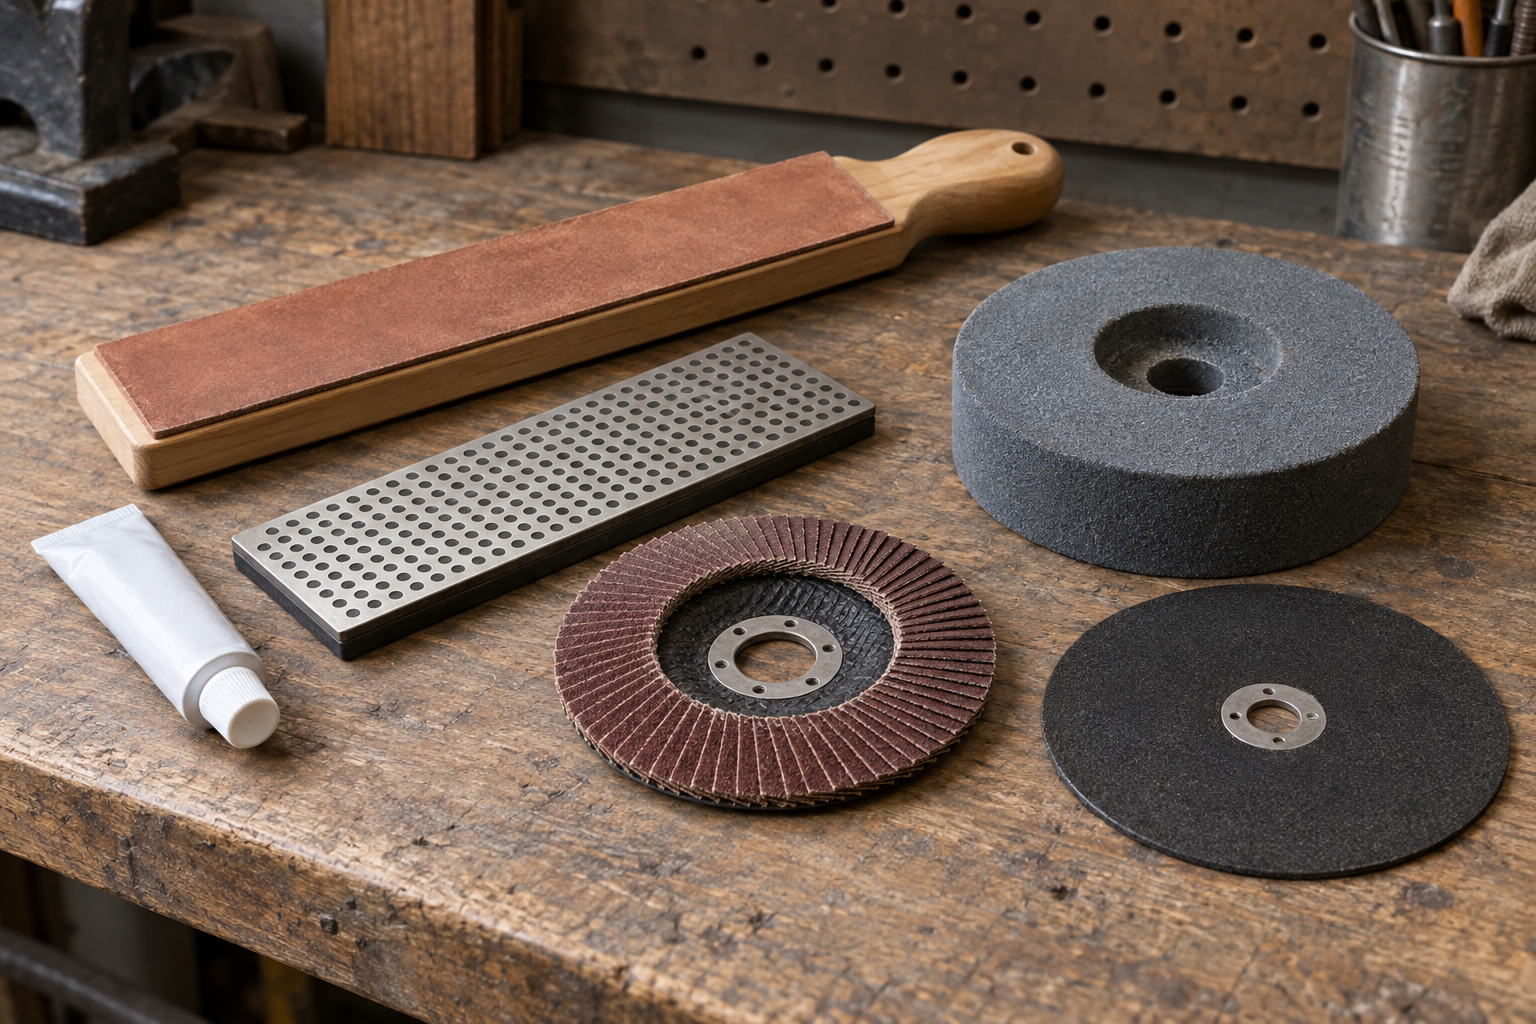
A flap disc usually removes weld metal with less gouging than a standard grinding wheel, especially when you’re blending a bead into thin or visible steel. Its layered abrasive flaps offer more control and a smoother finish. A grinding wheel is faster for knocking down a large, proud weld on thick stock, but it removes material aggressively and can leave deep hollows if you tilt or linger.
As an Amazon Associate we earn from qualifying purchases at no extra cost to you.


The short answer
Choose a flap disc for controlled weld blending, thinner work, and a finish that needs less cleanup. Choose a grinding wheel when speed matters more than surface finish and the workpiece has enough thickness to tolerate a heavier cut.
Neither accessory is gouge-proof. The operator’s angle, pressure, and time in one spot matter as much as the disc. If you are new to grinding, a flap disc is generally more forgiving—but it can still round edges, thin a plate, or remove too much metal.
Why the cut feels different
A grinding wheel is a thick, rigid abrasive wheel. Its edge concentrates force into a relatively small contact area, so it can remove weld metal quickly. That same concentrated cut makes it easy to dig into the parent metal. A worn wheel, excessive pressure, or a steep angle can make the cut uneven.
A flap disc is made from overlapping abrasive flaps attached to a backing plate. The flaps wear away gradually, exposing fresh abrasive, and flex slightly against the work. Used with the disc face at a shallow angle, it spreads the cut over a broader area and makes it easier to blend the weld toe without carving a trench.
That broader contact is a practical advantage, not a guarantee of a flat surface. Pressing hard or holding the disc in one place can still create a low spot. On thin sheet, a flap disc can also generate enough heat to warp the work.
Flap disc vs. grinding wheel
| Factor | Flap disc | Grinding wheel |
|---|---|---|
| Weld removal | Moderate; suited to blending and controlled removal | Fast; suited to heavy weld buildup |
| Gouging risk | Lower when held flat and moved steadily | Higher, especially with the edge or excessive pressure |
| Finish | Typically smoother; may be ready for a finer abrasive | Coarser; often needs a second finishing step |
| Best work | Thin or visible steel, weld toes, general cleanup | Thick stock, large beads, fast roughing |
| Trade-off | Slower on heavy welds; wears during blending | Less forgiving; can remove parent metal quickly |
Which one should you buy?
For one general-purpose angle-grinder accessory for weld cleanup, start with a 4½-inch, 40-grit flap disc. It is aggressive enough for many ordinary beads but easier to control than a hard grinding wheel. Grit ratings vary by task: 40 grit cuts more quickly, while 60 or 80 grit leaves a finer surface but takes longer to remove substantial weld.
Buy a grinding wheel if you regularly remove large, raised beads from thick steel and need speed. A depressed-center metal grinding wheel is the conventional choice for that roughing work. It is also a sensible, cheaper option when a coarse finish is acceptable or you will follow with another operation. Don’t buy one expecting it to leave a clean, flush surface without practice.
For the most control, remove most of a large bead with the wheel, stopping short of the base metal, then switch to a flap disc for blending. This two-step approach costs more in consumables and time spent changing accessories, but it limits how long the aggressive wheel is near the workpiece surface.
How to reduce gouging
Use the tool manufacturer’s recommended accessory and operating speed; never exceed the disc’s marked maximum RPM. Check that the accessory fits the grinder and is rated for metal. Keep the guard installed, wear eye and hearing protection, and use a face shield over safety glasses. Sparks can ignite dust, fuel, or nearby materials.
Clamp the work securely. Start with light pressure and keep the disc moving. For blending with a flap disc, hold it at a shallow angle—often around 5 to 15 degrees to the surface—and use broad, overlapping passes. Avoid rocking onto the rim or dwelling at the weld toe. With a grinding wheel, follow its instructions and use only the intended grinding face; don’t side-load a wheel that is not designed for it.
Stop frequently and inspect the weld and surrounding metal. A few short passes are easier to correct than one long, heavy cut. If the workpiece is thin, let it cool between passes. Discoloration, a growing low spot, or a sharp groove at the weld edge means you are removing too much parent metal; stop and reassess rather than trying to erase the damage with more grinding.
When neither is the right choice
If you only need to remove light spatter or smooth minor scratches, a less aggressive surface-conditioning disc may preserve more base metal, though it will not quickly flatten a substantial bead. For a cosmetic finish, plan on finer abrasives after the weld is blended.
Do not grind a weld that is part of a safety-critical structure simply to make it look flush. Removing the weld can weaken the joint, and a visual finish does not establish weld quality. If the joint’s strength matters, follow the applicable procedure or ask a qualified welder before removing material.